Vendor-neutral by design
We’re not limited to a single equipment line or vendor — we design solutions using the best-fit technology for your specific product and production goals.
Most food and beverage manufacturers don’t fail because the product isn’t good enough — they either can’t afford to start, or don’t know where to.
Efficient Food Solutions is a food manufacturing automation practice serving small and mid-sized food and beverage manufacturers. We exist to close the gap between a working product concept and a reliably industrialized production operation.
The gap
Equipment vendors sell equipment, not your product. General consultants look at specs, not ingredients. By the time a growing brand realizes they needed to consider both from the start, they are already behind.
That’s the gap Efficient Food Solutions exists to close.
How we work
We work with small and mid-sized food and beverage manufacturers at every stage of the journey from idea to industrialization. Start wherever you actually are.
EvaluatetoEfficient
Find what’s slowing your line down — and fix it, without buying equipment you don’t need.
You don’t always need a new, faster machine to increase productivity. We look at your whole process to try to save you money before you start spending it.
BenchtoBatch
Turn your recipe into a repeatable, machine-ready process.
Going from your kitchen to industrial batch sizes isn’t always straightforward. When you put product through a machine, you sometimes need to make changes. We have the people to help bring your product from the kitchen to the market.
ProducttoPallet
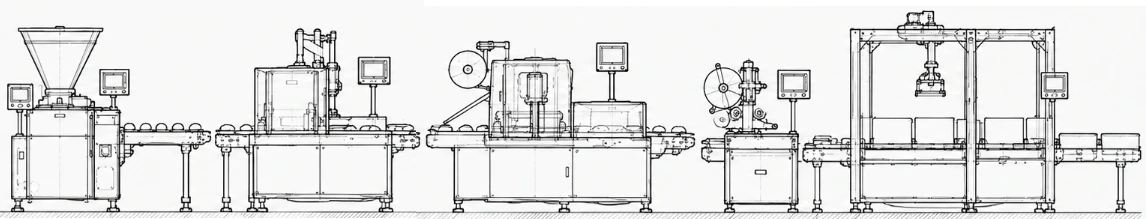
Design and spec the right production line — sized to your volume, not a vendor’s quota.
We look at your process from front to back and make sure we don’t just move the bottleneck.
Man PowertoManager
Integrate your new line, keep it running, and hand you back full control.
We’re flexible on the handoff and scope. Not everyone has the same experience, so every sales cycle shouldn’t be the same. Let’s talk about where the finish line is together.
How we sell
We don’t commit to equipment that puts our interests ahead of yours, and we don’t disappear after handoff — but we try to enable you to not need us to stay. Every engagement is built around one goal: leaving you more capable and more in control than we found you.
“Any sale is better than no sale” is not the way we work. We’re comfortable saying “we don’t think you’re ready for us yet.”
Why it matters
Automation isn’t just about speed. Slow is smooth, and smooth is fast. It’s about everything working in a flow.
This protects product consistency, strengthens food safety compliance, reduces labour strain, and gives you the traceability data regulators and retail partners increasingly expect. Our job is to make that transition possible.
Our work
Over the past decade, we’ve provided automated food production solutions for organizations across the industry, including:
Why us
We’re not limited to a single equipment line or vendor — we design solutions using the best-fit technology for your specific product and production goals.
Food production and industrial engineering. Deep electrical expertise combined with food-industry specialization, so the design accounts for food safety, throughput, and how a working plant actually runs.
Diagnosing an underperforming line, helping a recipe survive the jump from bench to batch, designing a line from scratch, or stepping in after an automation project has gone sideways.
We don’t disappear after handoff — but we try to enable you to not need us to stay. You end up more capable and more in control than we found you.
Common questions
Book a call, and we can determine where you are and where you could go.